




Reviews and corrects ledger-to-subledger alignment in D365 by fixing posting configurations, inventory profiles, reconciliation logic, GL mapping, and critical reporting procedures.
In Stock Is Not Line-Ready
Posted on: November 5, 2026 | By: Heather Zhu | Microsoft Dynamics AX/365, Microsoft Dynamics AX/365|Microsoft Dynamics Manufacturing
N13 / From Warehouse to Work Cell
The D365 handoff that holds up production, and how to find it before adding more inventory or more software.
By Logan Consulting | November 4, 2026 | 5-minute read
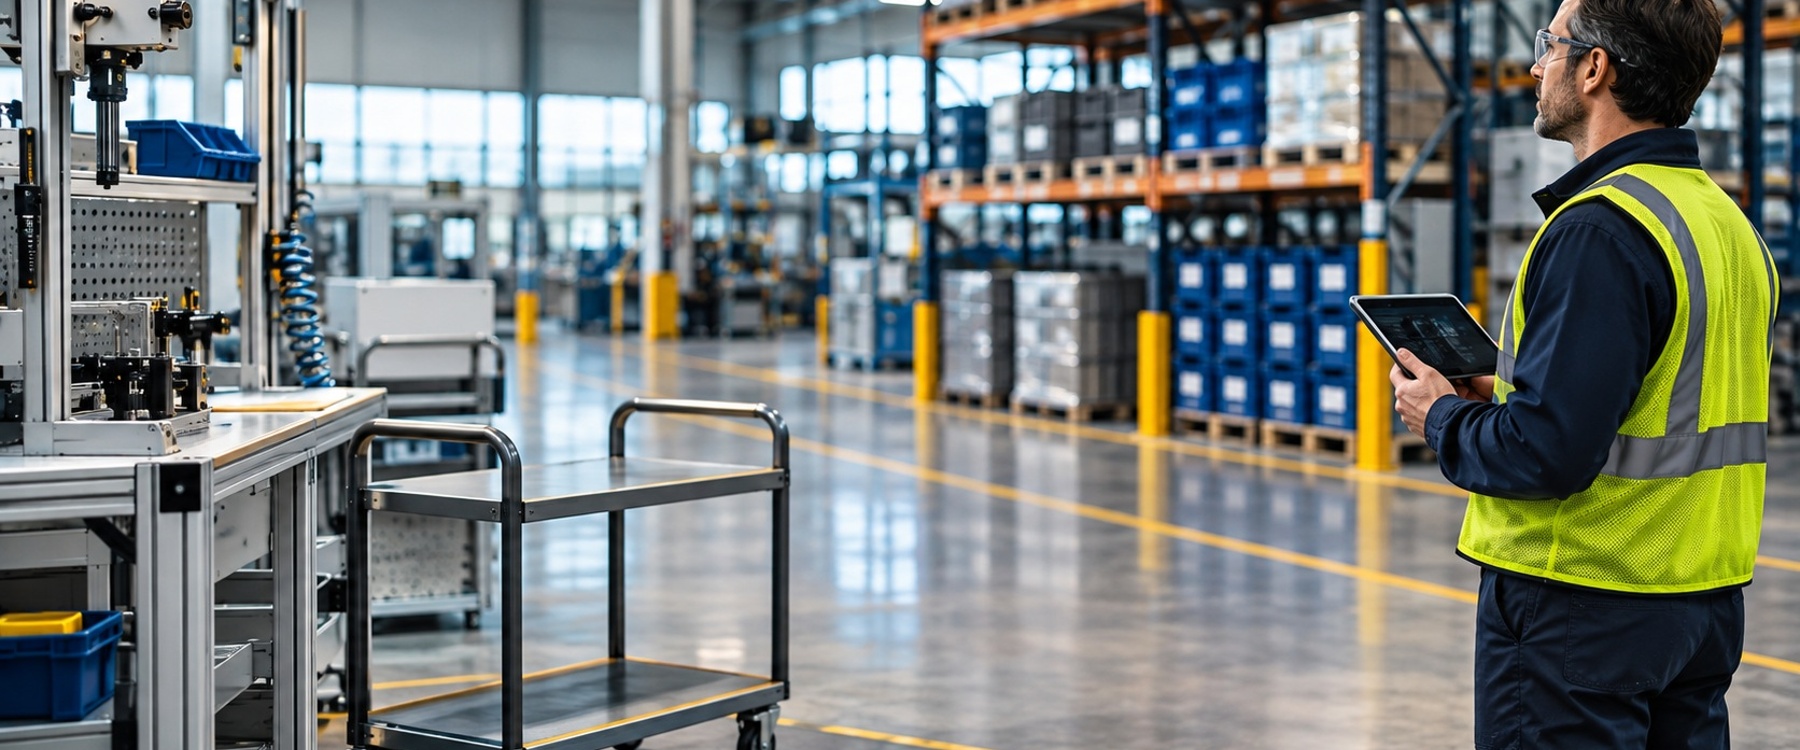 The gap between “in the warehouse” and “ready at the operation.” AI-generated conceptual photograph; not a customer facility.
At 6:55 a.m., the planner has released the production order. The inventory report shows plenty of material. The line supervisor is still waiting for it. Everybody has a green light. Nobody has the parts.
In this illustrative scene, the factory does not have a purchasing problem. It has an unfinished handoff. Buying more stock would make the inventory report more reassuring without making the line any more ready.
Logan’s position: diagnose the movement between warehouse availability and production readiness before changing the inventory policy. The useful question is not just “Do we have it?” It is “What still has to happen before this operation can use it?”
Released is permission, not proof.
In Dynamics 365 Supply Chain Management, Released authorizes a production order for execution. It does not certify that every component has arrived beside the machine. Raw-material picking also depends on reservations and the configured warehouse process.1
Material release is a separate decision. The Production line release parameter controls whether bill-of-materials (BOM) and formula lines release with the production order or through a batch job or manual action. Stock already at the production input location follows a different path from stock that still needs warehouse movement.2
That distinction reaches the operator’s screen. For WMS-enabled materials, the production floor execution interface’s Reserve material dialog shows physically available inventory at the production input location, not every unit sitting elsewhere in the warehouse.6
Find the queue before blaming the team.
Open the Production floor management workspace. Its three material-exception tiles separate the investigation:3
| D365 tile | The next question |
|---|---|
| Unreleased material lines needing attention | Has the component requirement reached the warehouse process? |
| Unprocessed waves needing attention | Has released demand been processed into picking work? |
| Open warehouse work needing attention | Has the required warehouse task been completed? |
Source: Microsoft Learn. Questions are Logan’s diagnostic prompts, not additional D365 settings.3
Check the workspace date and the Production unit, Resource group and Resource filters in Configure my work space. These affect which overdue or due material lines appear. An empty tile is not a universal all-clear. Drill into the underlying lines and confirm the scope.3
Then give the exception an owner. A planner, wave coordinator and warehouse supervisor may own different steps. Do not turn one missing handoff into three departments repeating the same investigation.
The Management Question
Which handoff is waiting, who owns it, and what evidence closes it?
Rehearse one component, not the whole factory.
Use a sandbox with the production and warehouse owners, normal business-role permissions, and an item and warehouse configured for warehouse management processes. Check the production input location, raw-material wave setup, work template and location directives. These are existing D365 controls, not a reason to buy an AI agent.1,4
Build an illustrative order requiring 240 units of one component. Put sufficient eligible stock in a bulk location and none at the production input location. Reserve the required quantity. Use a controlled manual material-release setup and a wave that is not automatically processed, so the team can observe each handoff.
At Production control > Setup > Production parameters, record the Production line release setting. From Production control > Production orders > All production orders, select the order, then Warehouse > Release to warehouse. Inspect the component quantities rather than relying on the production-order status.2
Follow the released line into its production wave, process and release that wave as required by the configuration, then complete the resulting raw-material picking work through the approved warehouse flow. Retain the order, component, wave and work references. Verify the destination and physical quantity before calling the component line-ready.1,3,4
The Success Test
With Manual flushing in this sandbox, confirm all 240 required units reach the input location and the corresponding movement work is complete. Inventory movement is not a consumption posting.5
Now repeat with the wave deliberately left unprocessed. The test passes when the team finds the correct exception, assigns the next action and resolves it without a duplicate move. As a separate visibility check, change the workspace date or resource filter and explain why the displayed queue changes. Restore the settings afterward.3
These are proposed acceptance tests, not results from a Logan customer or an executed tenant test. Verify the target build, reservations, dimensions, warehouse design and existing work policies. Some configured scenarios intentionally do not create movement work; missing work is not automatically a defect.9
Do not fix the queue by changing the accounting.
Keep consumption timing out of the experiment unless it is explicitly in scope. With Available at location flushing, material can be automatically consumed when registered as picked; the generated picking list is posted by a batch job. That can affect inventory and work in progress before an operator physically uses the material. It is not interchangeable with Manual flushing.5
Likewise, picking a whole pallet is not the same decision as making a line ready. Logan’s earlier over-picking guide covers that separate handling-policy question. Diagnose the stalled step before changing how much material moves.7
Measure the wait that disappears.
Track elapsed time from material release to completed movement, minutes of production delay attributed to material handoffs, and repeat manual touches. Pair those measures with safeguards: no duplicate moves, no unauthorized stock substitutions, no loss of tracking detail and no unexplained consumption postings.
Start with one line, one shift and one accountable owner for each queue. Compare similar orders before and after the change. A quieter screen is not the result; a reliable handoff is.
Bring Logan one recurring “in stock, but not here” example. We can help trace the D365 records, test the handoff and decide whether the fix belongs in configuration, execution or ownership.8
Remember One Thing
Inventory availability is a quantity. Production readiness is a completed handoff.
Sources and scope
- Microsoft Learn: Release production orders
- Microsoft Learn: Release BOM and formula lines to the warehouse
- Microsoft Learn: Visibility into material exceptions
- Microsoft Learn: Work with location directives
- Microsoft Learn: Control raw material consumption by using flushing principles
- Microsoft Learn: How workers use the production floor execution interface
- Logan Consulting: Understanding Over-Picking in Microsoft Dynamics 365 Supply Chain Management (September 11, 2023)
- Logan Consulting: Contact our team
- Microsoft Learn: Work policies
Verified November 4, 2026. This article covers standard Supply Chain Management warehouse/production functionality. No new release, measured customer result, tenant test or separate AI/partner license is claimed. Confirm your configuration and access before changes.